



How Flexible Biomanufacturing Capacity Supports Uncertain Demand
Introduction
Uncertain demand is reshaping biopharma investment, making rigid production models increasingly risky. Flexible biomanufacturing capacity helps leaders balance speed, compliance, cost, and supply continuity.
For enterprise decision-makers, the central question is rarely whether flexibility has value. The harder question is how much capacity to own, reserve, automate, or outsource.
Clinical trial outcomes, funding cycles, regulatory timing, regional access, and competitive launches can change product demand faster than traditional facility plans can respond.
A facility designed around one forecast may become underutilized after a program delay. Conversely, constrained capacity can delay pivotal trials, launch readiness, and revenue realization.
The strongest capacity strategy therefore treats manufacturing infrastructure as a portfolio of options, rather than a fixed asset built around a single commercial assumption.
Flexible biomanufacturing capacity does not mean accepting operational compromise. It means designing equipment, workflows, quality systems, and supplier relationships for controlled adaptation.
This article explains how decision-makers can evaluate flexible capacity, identify its economic value, manage compliance risk, and select an operating model suited to uncertainty.
Why Demand Uncertainty Creates a Capacity Problem
Biopharma demand uncertainty begins long before commercial launch. It is embedded in early clinical attrition, variable enrollment, changing dosage assumptions, and evolving portfolio priorities.
Even successful therapies may follow uneven adoption curves. Reimbursement decisions, physician confidence, patient identification, distribution constraints, and competitor activity can materially alter initial demand.
Cell and gene therapies introduce additional uncertainty because patient-specific workflows, site readiness, vein-to-vein timing, and limited treatment populations complicate conventional volume planning.
Biologics manufacturers also face changing batch requirements. A pipeline may shift from small clinical lots to larger commercial batches rapidly after positive data or accelerated approval.
Traditional stainless-steel facilities can deliver scale and long asset lives, but they usually require long construction schedules, product-specific validation, and substantial committed capital.
That model works best when demand is predictable, product volumes are high, and the company has confidence that a process will remain commercially relevant for years.
It becomes less attractive when multiple assets compete for limited internal capacity. A delayed molecule can leave expensive suites idle while another program requires urgent slots.
Flexible capacity protects against this mismatch by allowing companies to increase, decrease, reassign, or reserve production resources without rebuilding the entire manufacturing network.
The strategic benefit is optionality. Leaders can preserve the ability to respond to favorable events while limiting exposure to forecasts that may never materialize.
In practice, flexibility must be measured across time, scale, product compatibility, quality readiness, labor availability, and commercial contracting, not merely vessel volume.
What Flexible Biomanufacturing Capacity Actually Includes
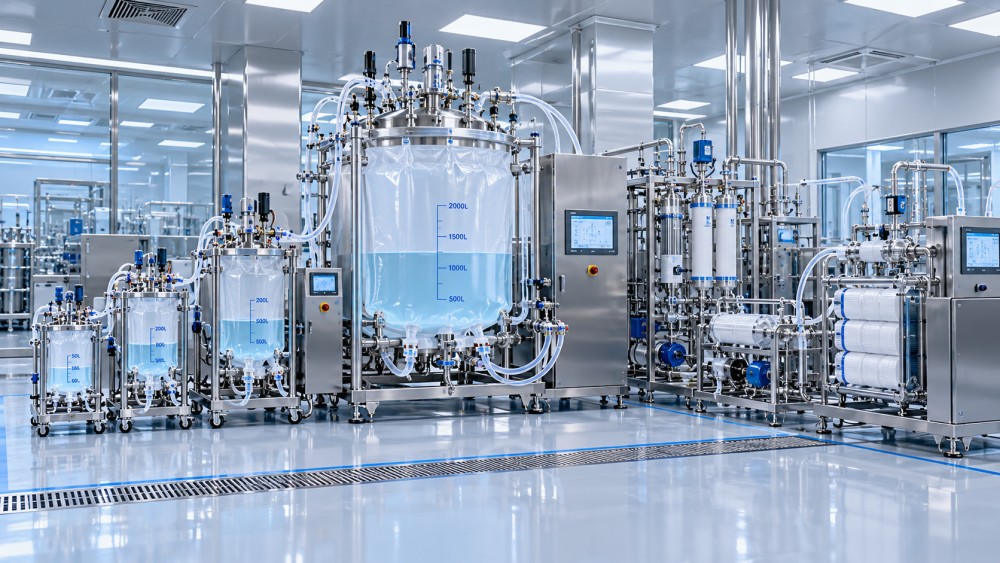
Flexible biomanufacturing capacity is often associated with single-use bioreactors, but a useful strategy extends across upstream, downstream, analytical, digital, and supply-chain operations.
Upstream flexibility begins with scalable bioreactor platforms. Companies can use compatible vessels across development, clinical, and commercial stages while maintaining comparable process control principles.
Single-use systems reduce cleaning validation requirements and shorten product changeovers. They are particularly valuable for multiproduct facilities, lower-volume biologics, and rapidly changing portfolios.
However, disposable technology is not automatically flexible. Film availability, connector standardization, mixing performance, waste handling, and extractables assessments must be addressed early.
Downstream operations frequently become the true bottleneck. Centrifugation, depth filtration, tangential flow filtration, chromatography, and virus clearance steps require coordinated throughput planning.
Modular downstream skids can improve adaptability when they support different process scales, flow paths, and chromatography configurations without creating uncontrolled validation complexity.
Automated liquid handling and digital batch execution create another layer of flexibility. They reduce manual variation while allowing standardized workflows to be deployed across products or sites.
Analytical capacity matters equally. LC-MS systems, process analytics, and release testing workflows must scale with manufacturing output or production gains may simply move delays downstream.
Flexible capacity also includes external options. Qualified contract development and manufacturing organizations can provide surge capacity, specialized capabilities, and geographic redundancy when internal resources are constrained.
The best operating model combines physical assets with qualified alternatives. This allows management to make capacity decisions based on evidence instead of urgency or sunk-cost pressure.
Which Business Problems Flexibility Can Solve
Flexible capacity is most valuable when it solves a defined business problem. It should not become a vague technology preference or an expensive response to uncertainty.
One common use case is clinical acceleration. A company with positive Phase II data may need engineering, registration, or pivotal batches before permanent commercial capacity exists.
Another use case is portfolio volatility. A multiproduct manufacturer can reassign suites when priorities change, rather than allowing a single delayed asset to consume dedicated space.
Flexible infrastructure also supports lifecycle management. Process improvements, new presentations, regional supply requirements, and additional indications can be introduced with fewer disruptive facility modifications.
For emerging biotech companies, the primary value may be capital preservation. Flexible models delay irreversible investment until clinical and commercial evidence becomes more reliable.
For established pharmaceutical companies, the greater value may be responsiveness. Existing networks can use adaptable capacity to bridge shortages, launch new assets, or manage demand spikes.
In vaccines and infectious disease programs, speed has particular importance. Demand may emerge suddenly, while the window for clinical, public health, and commercial impact remains limited.
For biosimilars, flexibility can reduce the risk of committing capacity before pricing, tender outcomes, and market access conditions are fully understood across target regions.
In CGT, modular and closed processing systems can support decentralized or regional manufacturing models, although chain-of-identity controls and site comparability require rigorous governance.
Executives should define the specific uncertainty they need to absorb. Demand risk, timing risk, process risk, supply risk, and portfolio risk require different flexibility mechanisms.
How to Evaluate the Economics Beyond Capital Expenditure
A flexible platform can appear more expensive per batch than a dedicated facility. That comparison is incomplete when it ignores utilization, delay costs, and strategic optionality.
Decision-makers should begin with total cost of ownership. This includes capital expenditure, consumables, utilities, facility operations, labor, maintenance, qualification, waste, and quality oversight.
They should then model utilization across multiple demand scenarios. A facility that looks efficient at full capacity may become financially unattractive when operating significantly below its design rate.
Scenario analysis should include base, upside, downside, and delay cases. It should also consider whether competing pipeline assets could use the same manufacturing platform.
The cost of lost opportunity often exceeds visible operating costs. Missing a pivotal trial window or delaying launch supply can impair enterprise value and competitive position.
Capacity decisions should therefore include time-to-batch and time-to-market metrics. Faster availability may justify higher unit costs when it prevents material commercial or development delays.
Companies should also evaluate working-capital effects. Shorter campaigns, smaller inventories, and more frequent replenishment can reduce exposure to obsolete material and forecast error.
External capacity contracts need similar scrutiny. Reservation fees, minimum batch commitments, technology transfer costs, cancellation terms, and priority rights determine whether outsourced flexibility is genuine.
A useful investment case assigns value to avoided outcomes, including idle facilities, emergency outsourcing, supply interruption, delayed enrollment, and missed revenue during launch periods.
Flexibility creates value when the cost of preserving options is lower than the expected cost of being unable to respond. That is the core financial test.
How to Preserve GMP Compliance While Increasing Adaptability
Some leaders worry that flexible manufacturing will create a less controlled environment. In reality, well-designed flexibility can strengthen control by standardizing reusable operational patterns.
GMP compliance depends on validated processes, qualified equipment, documented change control, trained personnel, data integrity, and a quality system capable of governing variation.
Flexibility becomes risky when products are moved between platforms without comparability evidence. It also fails when rapid changeovers bypass cleaning, segregation, or documentation requirements.
Single-use technologies can simplify contamination control because they eliminate many shared-contact surfaces. Yet they require robust supplier qualification and lifecycle management for disposable assemblies.
Standardized equipment families help reduce validation effort. When controls, sensors, software, and operating ranges remain consistent, teams can apply proven knowledge more effectively.
Computerized system validation must be planned as part of flexibility. Automated batch records, recipe management, audit trails, and user access controls cannot be treated as late-stage additions.
Data architecture should support traceability across development, manufacturing, analytics, and release. This is especially important when products move among internal sites and external partners.
Quality teams need predefined decision rights for process changes. Clear comparability protocols prevent urgent commercial decisions from becoming uncontrolled technical changes under deadline pressure.
Regulatory expectations also favor science-based control strategies. Companies that understand critical quality attributes and process parameters can adapt more confidently without weakening oversight.
The practical goal is controlled adaptability: a manufacturing system that can change deliberately, document evidence clearly, and demonstrate consistent product quality after each change.
Choosing Between Internal Capacity, CDMOs, and Hybrid Models
There is no universally correct ownership model. The appropriate structure depends on pipeline maturity, technology complexity, demand visibility, internal expertise, and tolerance for external dependency.
Internal manufacturing offers direct control over scheduling, technical knowledge, workforce development, and quality culture. It can become attractive when demand is durable and utilization is high.
Its disadvantages are capital intensity and slower response to portfolio shifts. Building capacity too early may consume cash that would otherwise support clinical development or acquisitions.
CDMOs provide established infrastructure and experienced teams. They can reduce initial capital requirements and offer specialized services such as high-potency handling, viral vectors, or complex analytics.
Yet external capacity brings scheduling competition and technology-transfer risk. A contract does not guarantee operational priority unless capacity rights, governance, and escalation pathways are clearly defined.
A hybrid model often gives enterprise decision-makers the best balance. Core products or proprietary processes remain internal, while volatile demand and specialized requirements use qualified partners.
Hybrid networks should not be managed casually. Internal and external sites need aligned materials strategies, technical transfer standards, quality agreements, and data exchange procedures.
Companies should also avoid relying on a single external provider for critical supply. Geographic concentration, raw material dependencies, and provider capacity constraints can become serious business risks.
Dual sourcing is not always practical, especially for early-stage programs. But contingency planning should identify the evidence, timeline, and investment needed to activate alternatives.
The final choice should reflect the company’s risk profile. Ownership is valuable when control matters most, while access is valuable when uncertainty dominates the business case.
What Leaders Should Measure Before Committing Capacity
Capacity planning becomes more reliable when leaders use a focused scorecard instead of relying on a single forecast or a simple liters-per-year calculation.
Start with demand confidence. Measure the quality of clinical evidence, probability-adjusted volumes, expected timing, market access dependencies, and the consequences of forecast error.
Next, assess process maturity. A stable process with known yields and well-characterized critical parameters can be scaled more confidently than an evolving development-stage platform.
Utilization is essential, but average utilization can hide risk. Review peak demand, campaign lengths, changeover time, maintenance windows, and required buffer capacity separately.
Evaluate time-to-capacity from the moment demand changes. This includes equipment delivery, installation, qualification, technology transfer, raw material lead times, and workforce readiness.
Review supply-chain resilience for critical consumables, resins, filters, media, sensors, and disposable assemblies. Flexible facilities still fail when essential components are unavailable.
Assess talent capacity as carefully as equipment capacity. Experienced operators, automation engineers, validation specialists, and quality reviewers can become the actual limiting resource.
Finally, track decision reversibility. The more irreversible an investment, the stronger the supporting evidence should be before management commits capital and organizational attention.
Building a Practical Flexible Capacity Roadmap
A practical roadmap begins by segmenting the portfolio. Products should be grouped by modality, process similarity, demand confidence, commercial value, and manufacturing complexity.
Management can then identify common platforms suitable for shared upstream, downstream, analytical, or automation capabilities. Standardization creates the operational foundation for flexibility.
The next step is defining capacity bands rather than one fixed target. Each band should specify trigger points for internal expansion, external reservation, and contingency activation.
These trigger points should be tied to evidence, such as clinical milestones, confirmed purchase orders, reimbursement decisions, validated yields, or sustained utilization thresholds.
Companies should qualify critical external partners before an emergency occurs. Technology transfer and quality onboarding take time, particularly for complex biologics and advanced therapies.
Equipment selection should consider more than current throughput. Interoperability, data connectivity, operator ergonomics, service coverage, and platform compatibility affect long-term adaptability.
Leaders should fund digital infrastructure alongside physical equipment. Integrated scheduling, electronic batch records, equipment data, and inventory visibility support faster, defensible decisions.
Regular portfolio reviews are necessary because uncertainty changes. Capacity plans should be revisited after material clinical, commercial, regulatory, or supply-chain developments.
Conclusion: Flexibility Is a Strategic Capacity Discipline
Flexible biomanufacturing capacity is not simply a collection of disposable systems or smaller bioreactors. It is a disciplined approach to managing uncertainty without sacrificing control.
For enterprise decision-makers, the objective is to avoid two costly extremes: overbuilding against optimistic forecasts and underinvesting until supply limitations become irreversible.
The strongest strategies combine scalable equipment, capable downstream operations, automated quality systems, resilient supply chains, and qualified internal or external production alternatives.
Investment decisions should be based on scenario economics, time-to-capacity, compliance readiness, and the value of preserving options across a changing product portfolio.
When designed deliberately, flexible biomanufacturing capacity allows organizations to pursue growth with greater confidence, protect supply continuity, and scale innovation when evidence supports action.
Related News
- How to maintain product quality when scaling up a bioprocessOct 09, 2026Prof. Alistair Thorne
- What should you verify before choosing a bioprocessing equipment exporter?Oct 08, 2026Prof. Alistair Thorne
- How to preserve critical quality attributes during bioreactor scale-up process transferOct 07, 2026Prof. Alistair Thorne
- How flexible biomanufacturing capacity supports uncertain demandOct 10, 2026Prof. Alistair Thorne
Related News
- 00
0000-00
How to assess audit trails in analytical data integrity solutions - 00
0000-00
How to assess an automated liquid handling platform's throughput - 00
0000-00
How user licensing affects laboratory validation system pricing - 00
0000-00
When does pathogen sample processing require a Class III cabinet? - 00
0000-00
How secure data integrity systems support GMP audit readiness
Prof. Alistair Thorne
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.